The UK leader in Stud Welding and Refractory products
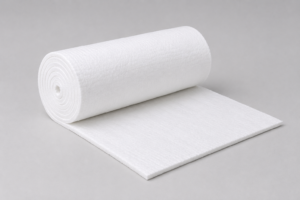
The Saffil® 72 Range is a family of premium polycrystalline wool (PCW) insulation products engineered for continuous operating temperatures up to 1600°C. Manufactured from high-purity mullite fibres containing approximately 72% alumina and 28% silica, Saffil 72 products provide exceptional thermal stability, chemical resistance and insulation performance in applications where conventional ceramic fibre and AES insulation materials reach their operating limits.
Designed for demanding thermal processing environments, Saffil 72 products deliver extremely low thermal conductivity, outstanding resiliency and excellent dimensional stability at elevated temperatures. Their high fibre content and low shot levels ensure consistent performance, enhanced insulation efficiency and reliable long-term operation in extreme heat-processing applications.
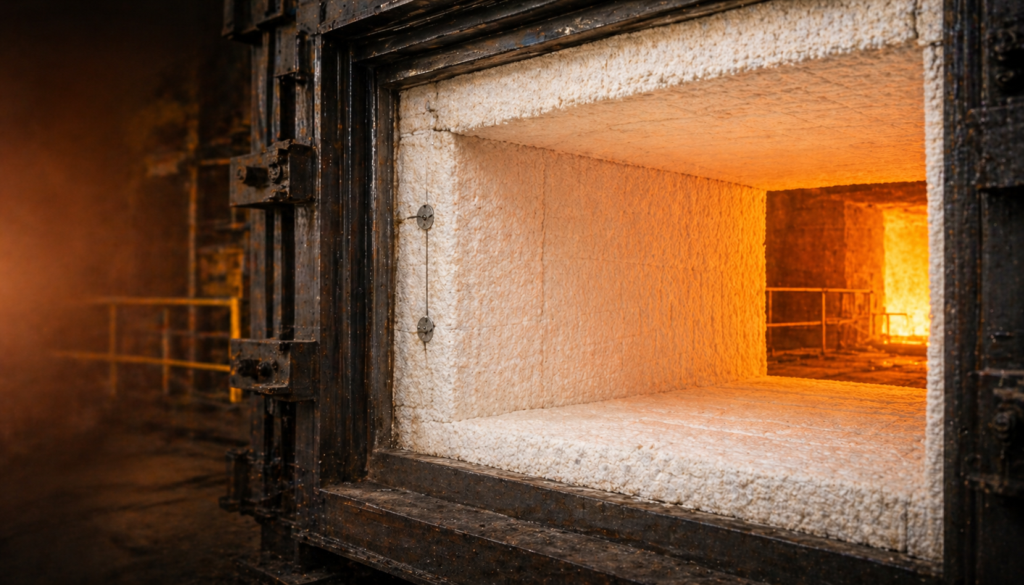
Available in multiple formats and densities, the Saffil 72 Range provides tailored solutions for iron and steel production, ceramics manufacturing, petrochemical processing, aerospace applications and advanced thermal management systems.
Saffil 72 products deliver exceptional performance in the most demanding high-temperature insulation applications.
| Property | Saffil 72 Bulk |
| Classification Temperature | 1600°C |
| Melting Point | >1870°C |
| Mean Fiber Diameter | 2-3.5 Microns |
| Typical Chemical Analysis (wt. %) | |
| Al2O3 | 72-75 |
| SiO2 | 25-28 |
| Trace | <0.5 |
| Property | Saffil 72 Blanket | Saffil 72+ Blanket | Saffil 72HD Blanket |
| Classification Temperature | 1600°C | 1600°C | 1600°C |
| Melting Point | >1870°C | >1870°C | >1870°C |
| Mean Fiber Diameter | 4-5 Microns | 6-7 Microns | 4-6 Microns |
| Typical Chemical Analysis (wt. %) | |||
| Al2O3 | 72 | 72 | 72 |
| SiO2 | 28 | 28 | 28 |
| Trace | <0.5 | <0.5 | <0.5 |
The Saffil 72 Range is used in extreme-temperature industrial processes where thermal stability, chemical resistance and insulation performance are required.
Saffil 72 products are specified across industries requiring insulation materials capable of maintaining performance in severe thermal environments.
Selecting the correct Saffil 72 product is essential for achieving optimum thermal efficiency, process reliability and service life in ultra-high-temperature applications. Factors such as operating temperature, atmosphere conditions, chemical exposure and thermal cycling should all be considered during specification.
Our technical team provides support across insulation design, material selection and thermal performance optimisation, helping ensure the most suitable Saffil solution is specified for your operating environment.
Speak with our technical specialists to discuss extreme temperature insulation requirements, furnace design and advanced thermal processing applications. We can assist with product selection, thermal calculations and application-specific specification guidance.